- Tel: +86 133 3836 0365
- Email: john@yxs-forging.com
Forged Ring Blanks for Gear Manufacturing China Suppliers Factory


Forged Ring Blanks for Gear Manufacturing China Suppliers Factory
Contact Us Now >
Download
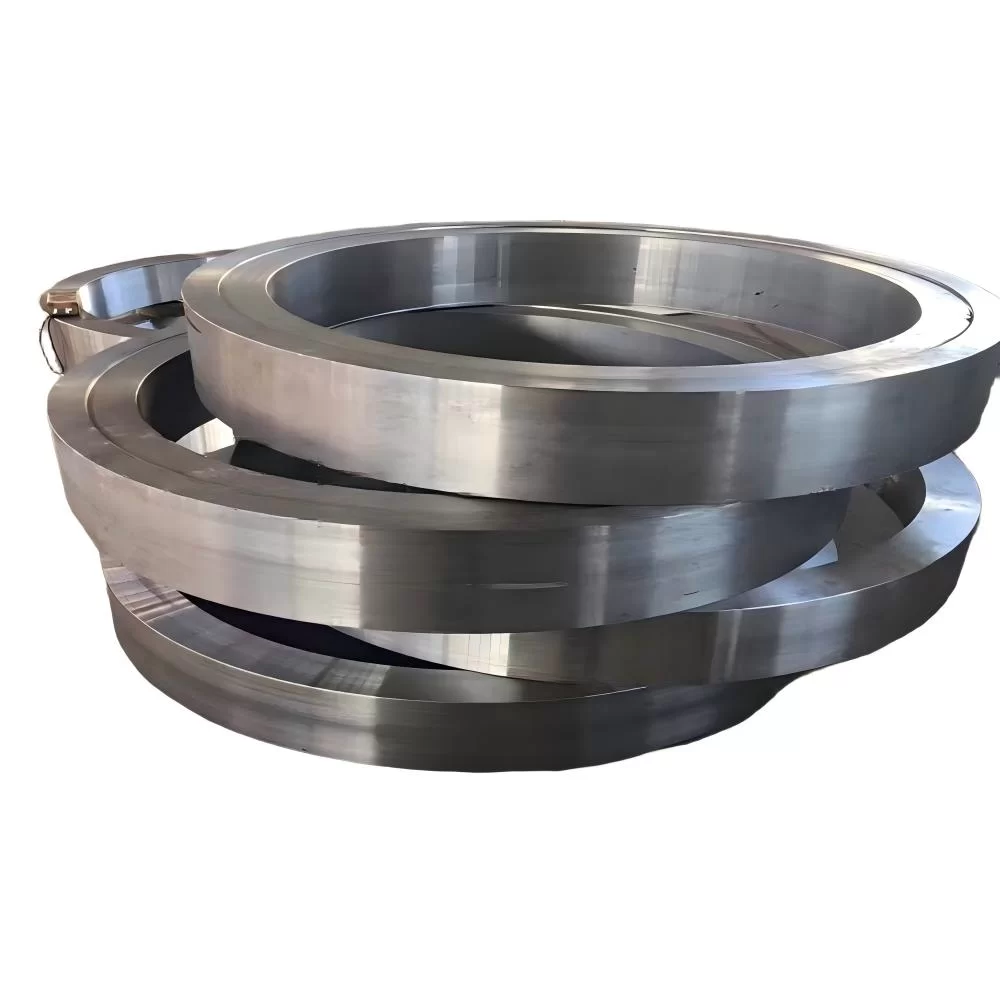
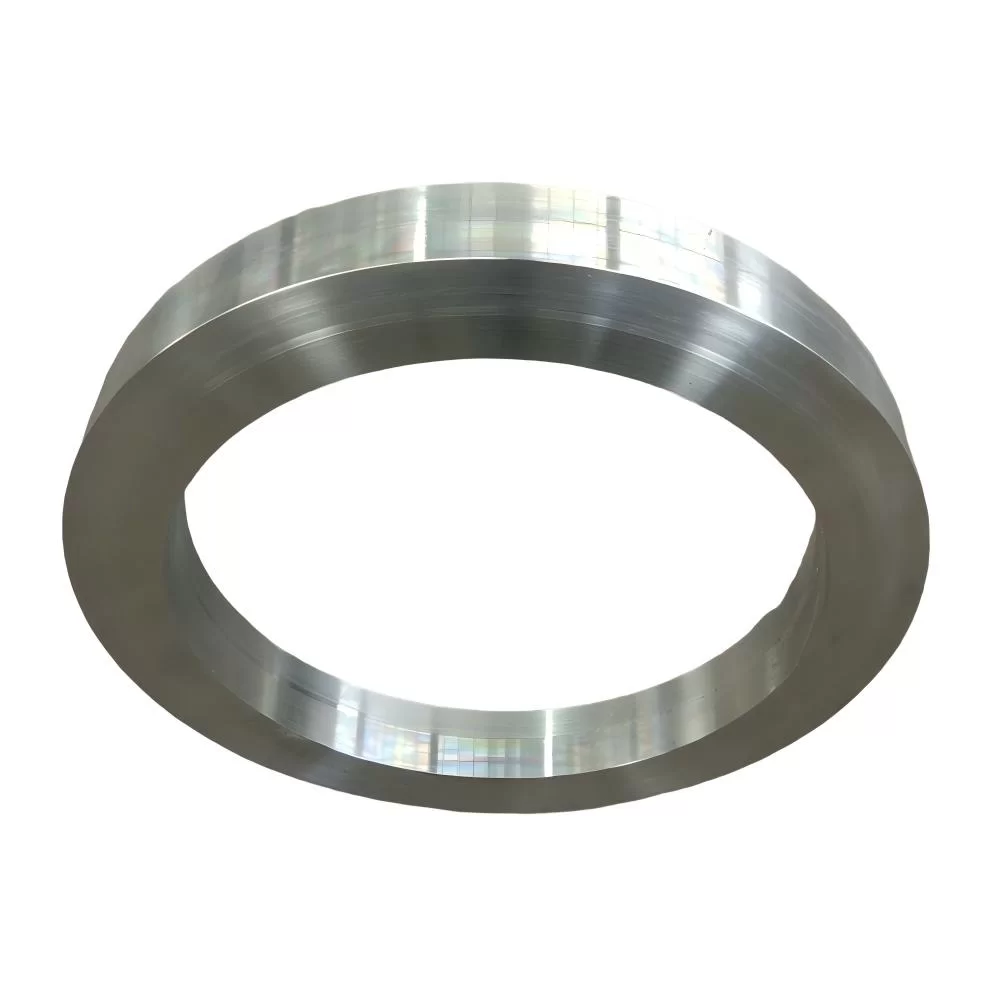
Our Forged Ring Blanks for Gear Manufacturing are high-performance semi-finished components engineered specifically for downstream precision machining. Designed for critical applications such as ring gears, internal gears, and complex transmission components, these blanks ensure controlled grain flow and superior structural integrity. Whether produced via open-die forging or seamless rolling, our rings provide the essential dimensional stock required to maximize strength while minimizing material waste during the final gear-cutting process.
To ensure seamless integration into your production line, we offer rigorous control over ring roundness, cross-sectional consistency, and heat-treatment responsiveness. This stability is critical for large-module gears where hobbing or gear milling accuracy depends entirely on the quality of the forged blank. From ultrasonic testing to custom machining allowances, our blanks are tailored to meet the most demanding industrial standards for heavy-duty machinery and automotive power trains.
Detailed Parameters
| Typical Materials | 42CrMo4, 34CrNiMo6, 20CrMnTi, or per customer drawing | Outer Diameter (OD) | 300mm to 6000mm |
|---|---|---|---|
| Maximum Height | ≤ 1000mm | Maximum Unit Weight | ≤ 25 Tons |
| Manufacturing Process | Open-die forging or Rolled ring forging | Supply Condition | As-forged / Normalized & Tempered / Rough Machined |
| Inspection Standards | UT (Ultrasonic Testing), Hardness Uniformity | Certification | EN 10204 3.1, Traceability List, Dimensional Report |
| Key Applications | Industrial Gearboxes, Reducer Rings, Slewing Rings | Available Services | Rough Turning, Quenching, Tempering, 3rd Party Inspection |
Key Advantages
Optimized Grain Flow
Controlled forging processes ensure continuous grain flow, significantly enhancing the fatigue strength and durability of finished gears.
Reduced Machining Waste
Precision-near-net shapes reduce the volume of material removed during hobbing, lowering tool wear and production costs.
High Dimensional Stability
Strict control over roundness and section consistency ensures stable performance during high-precision gear milling.
Custom Heat Treatment
Tailored normalizing, quenching, and tempering processes to achieve the exact hardness and microstructure required.
Rigorous UT Testing
Comprehensive Ultrasonic Testing levels ensure the internal integrity of the forging and the absence of critical defects.
Full Traceability
Every ring blank is accompanied by full material traceability and EN 10204 3.1 certification for quality assurance.
Product Gallery

Management Platforms
Material Sourcing
Strict selection of high-alloy steels ensuring purity and chemical consistency for gear applications.
Forging Precision
Advanced open-die and rolling equipment to achieve tight dimensional tolerances on large diameters.
Quality Monitoring
Real-time tracking of heat treatment parameters to ensure uniform hardness across the section.
Inspection Protocol
Multi-stage verification including UT, dimensional checks, and surface finish audits.
Logistical Coordination
Professional handling and packaging for oversized forged rings up to 25 tons.
Technical Support
Expert guidance on machining allowances and heat treatment response for specific gear modules.
Investment Return Comparison
| Comparison Metric | Cast Ring Blanks | Our Forged Ring Blanks |
|---|---|---|
| Structural Integrity | Prone to porosity/voids | Dense, refined grain structure |
| Mechanical Strength | Moderate; lower fatigue limit | Superior tensile & yield strength |
| Machining Waste | High due to oversized casting | Low due to near-net forging |
| Performance Life | Standard operational life | Extended life under heavy loads |
| Reliability | Variable consistency | Highly predictable & certified |
Frequently Asked Questions
Q: What is the main advantage of using a forged ring blank over a cast one for gears?
Forged ring blanks offer a controlled grain flow and higher density, which results in significantly higher fatigue strength and impact resistance compared to cast rings, which may contain internal porosity.
Q: Can you provide custom machining allowances for tooth cutting?
Yes, we can supply rough-machined rings with specific allowances on the ID, OD, and faces to ensure your downstream gear-cutting process is efficient and accurate.
Q: Which materials are most commonly used for gear forging blanks?
Depending on the application, we typically use high-strength alloy steels such as 42CrMo4, 34CrNiMo6, and 20CrMnTi to ensure optimal wear resistance and toughness.
Q: What quality documentation is provided with each shipment?
We provide a comprehensive documentation package including EN 10204 3.1 certificates, ultrasonic testing reports, dimensional inspection sheets, and full heat-traceability lists.
Q: How do you ensure the roundness of very large diameter rings?
We utilize precision rolling technology and rigorous post-forging heat treatments to minimize distortion, followed by precision rough turning to meet strict roundness specifications.
Q: Do you offer third-party inspection coordination?
Yes, we fully support and coordinate with third-party inspection agencies to verify material properties, dimensions, and NDT results before final shipment.
Ready to optimize your gear production with precision forgings?
Contact Us-
 Precision Hollow Main Shaft Forgings China Suppliers | Heavy Duty Rotating Parts FactoryHigh-performance hollow main shaft forgings from a leading China factory. Our suppliers provide precision engineered shafts for turbines and motors, offering reduced mass, UT 100 inspection, and superior structural reliability.
-
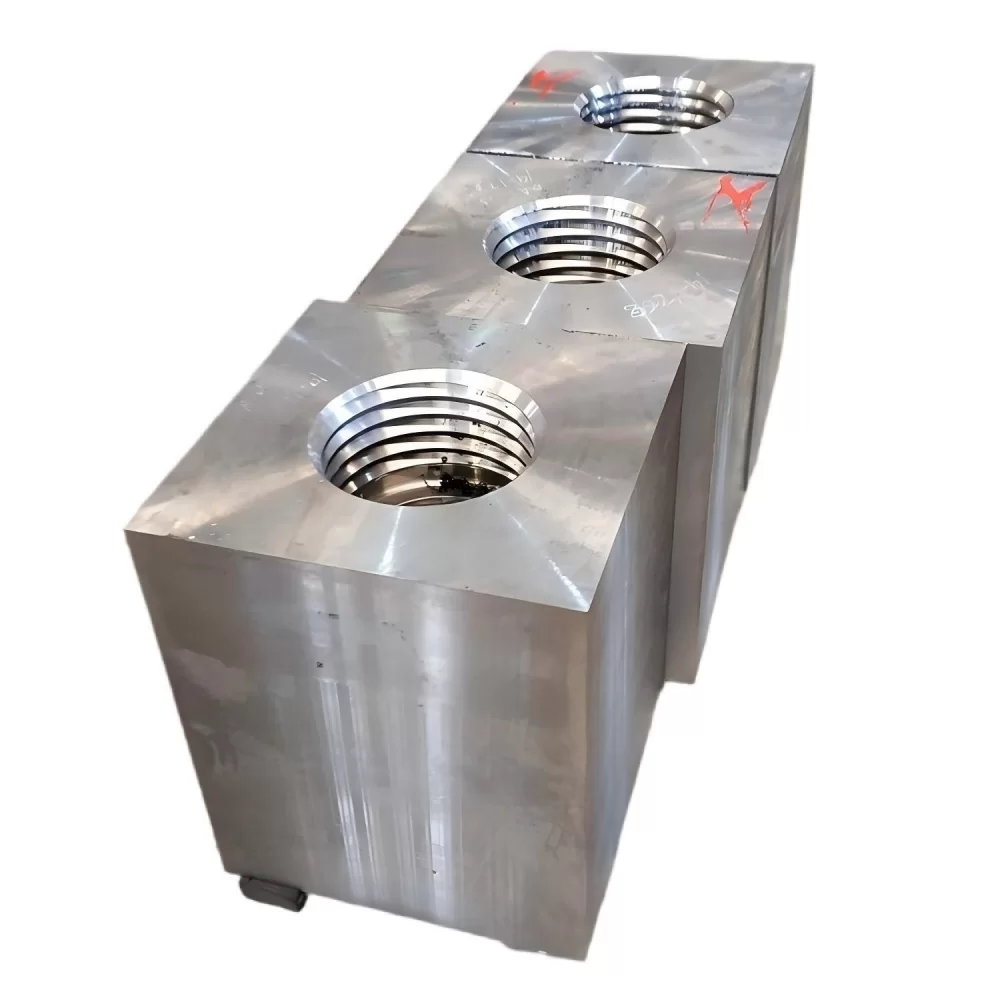 Forged Block for Machining
Forged blocks for machining are solid forged preforms supplied for subsequent machining into non-standard heavy parts and structural components.
-
 Custom Hollow Main Shaft Forgings China Factory | Professional Industrial SuppliersSource high-precision hollow main shaft forgings from our leading China factory. As expert suppliers, we deliver heavy-duty forged shafts with exceptional concentricity and structural integrity for rotating systems.
-
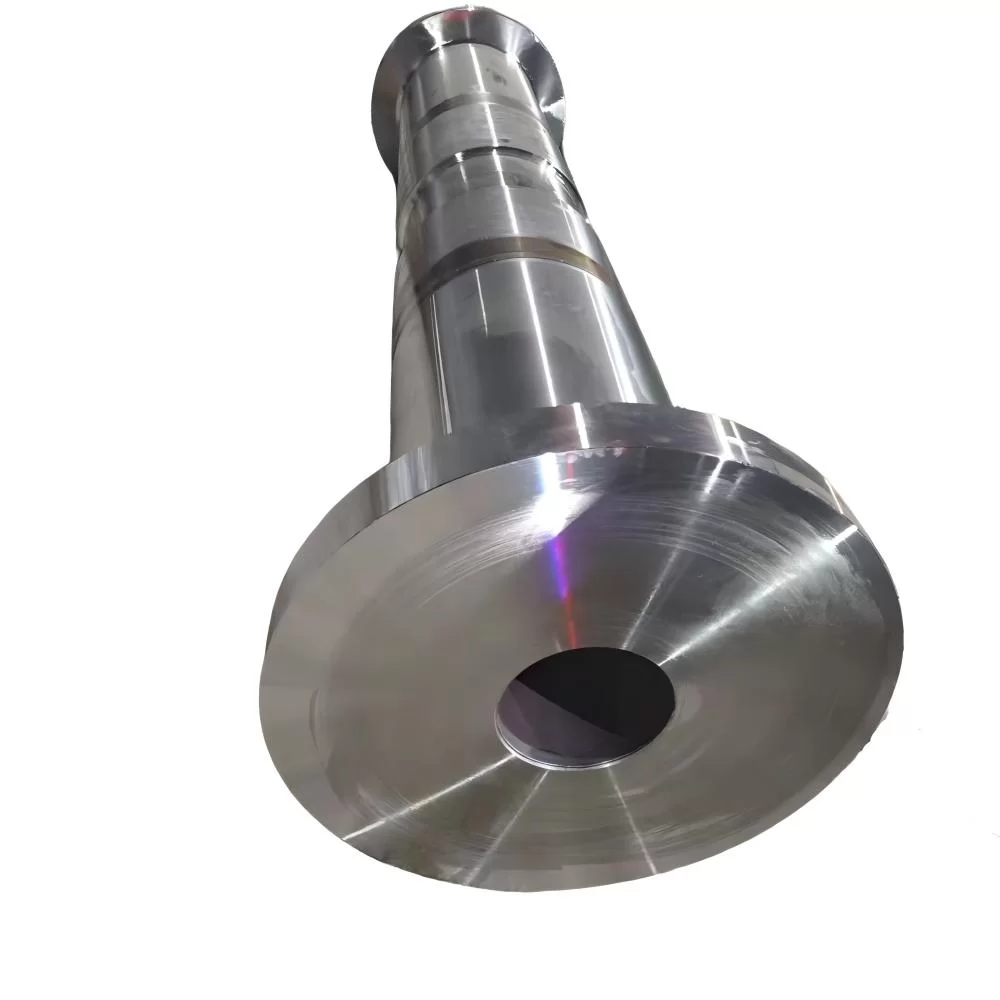 Precision Hollow Main Shaft Forgings China Factory and Leading SuppliersLooking for high-precision hollow main shaft forgings from a reliable China factory? Our professional suppliers provide heavy-duty forged shafts with superior concentricity and structural integrity for rotating systems.
-
 Custom Forged and Machined Ring
Custom forged and machined rings are produced for non-standard industrial applications that require both forged strength and drawing-based machining accuracy.
-
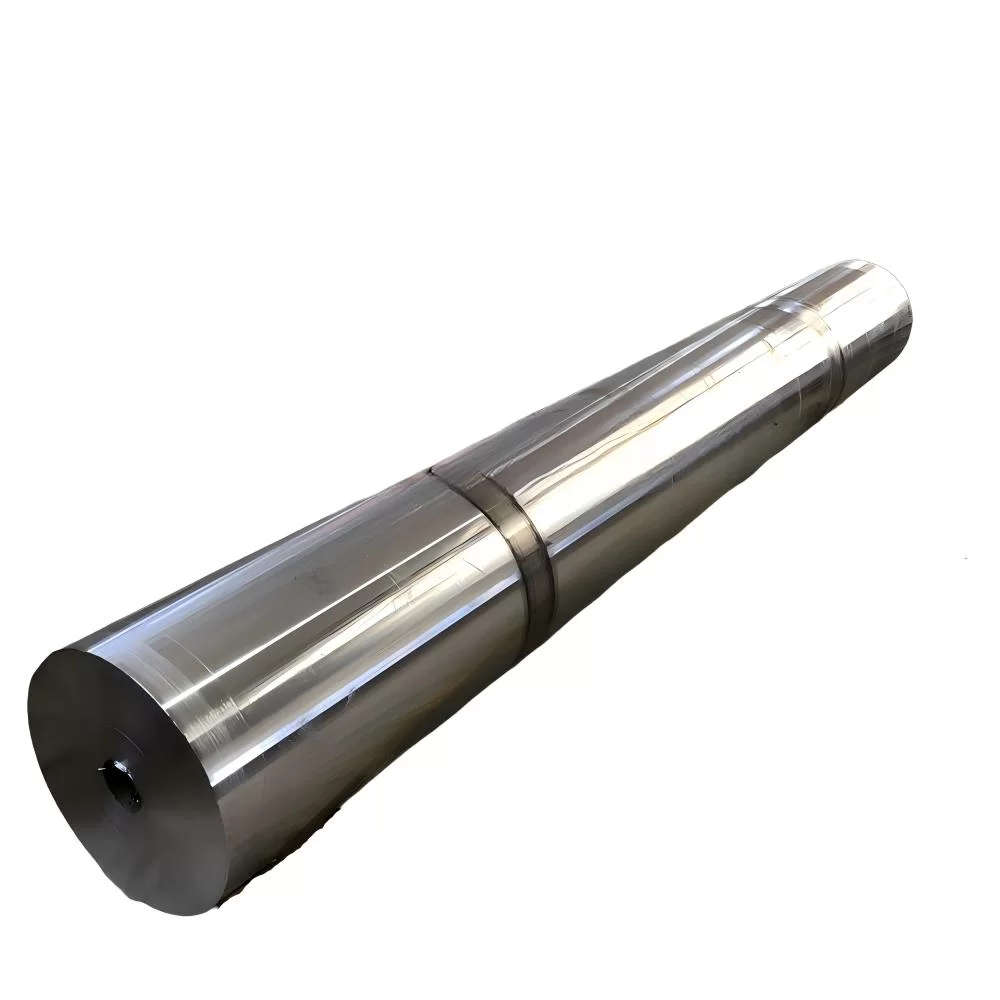 Crusher Main Shaft Forging
Crusher main shaft forgings are engineered for heavy crushing equipment where impact load resistance, section strength, and machining reliability are critical.
-
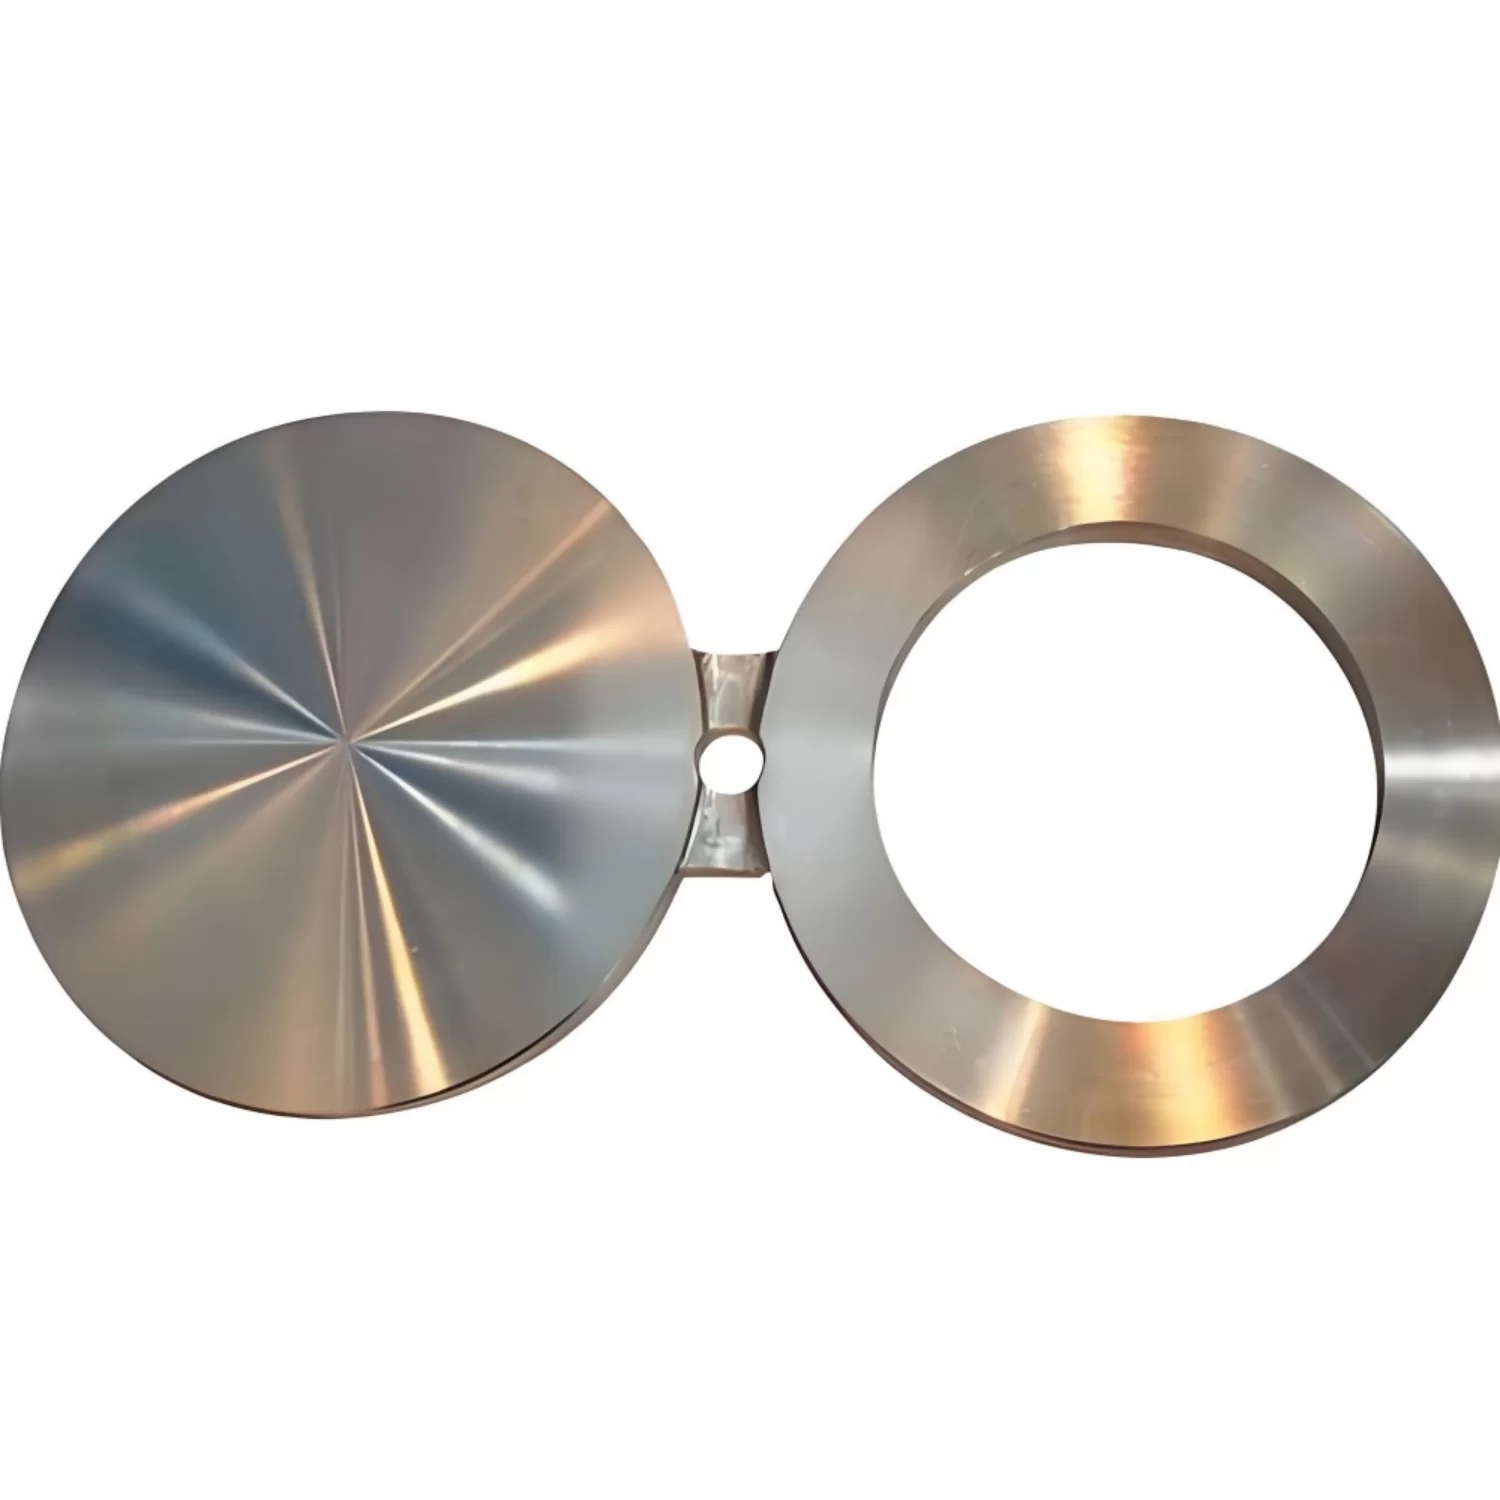 Spectacle Blind
s are line isolation components used in industrial piping systems to provide visible and reliable shut-off during maintenance, inspection, or process changeover.
-
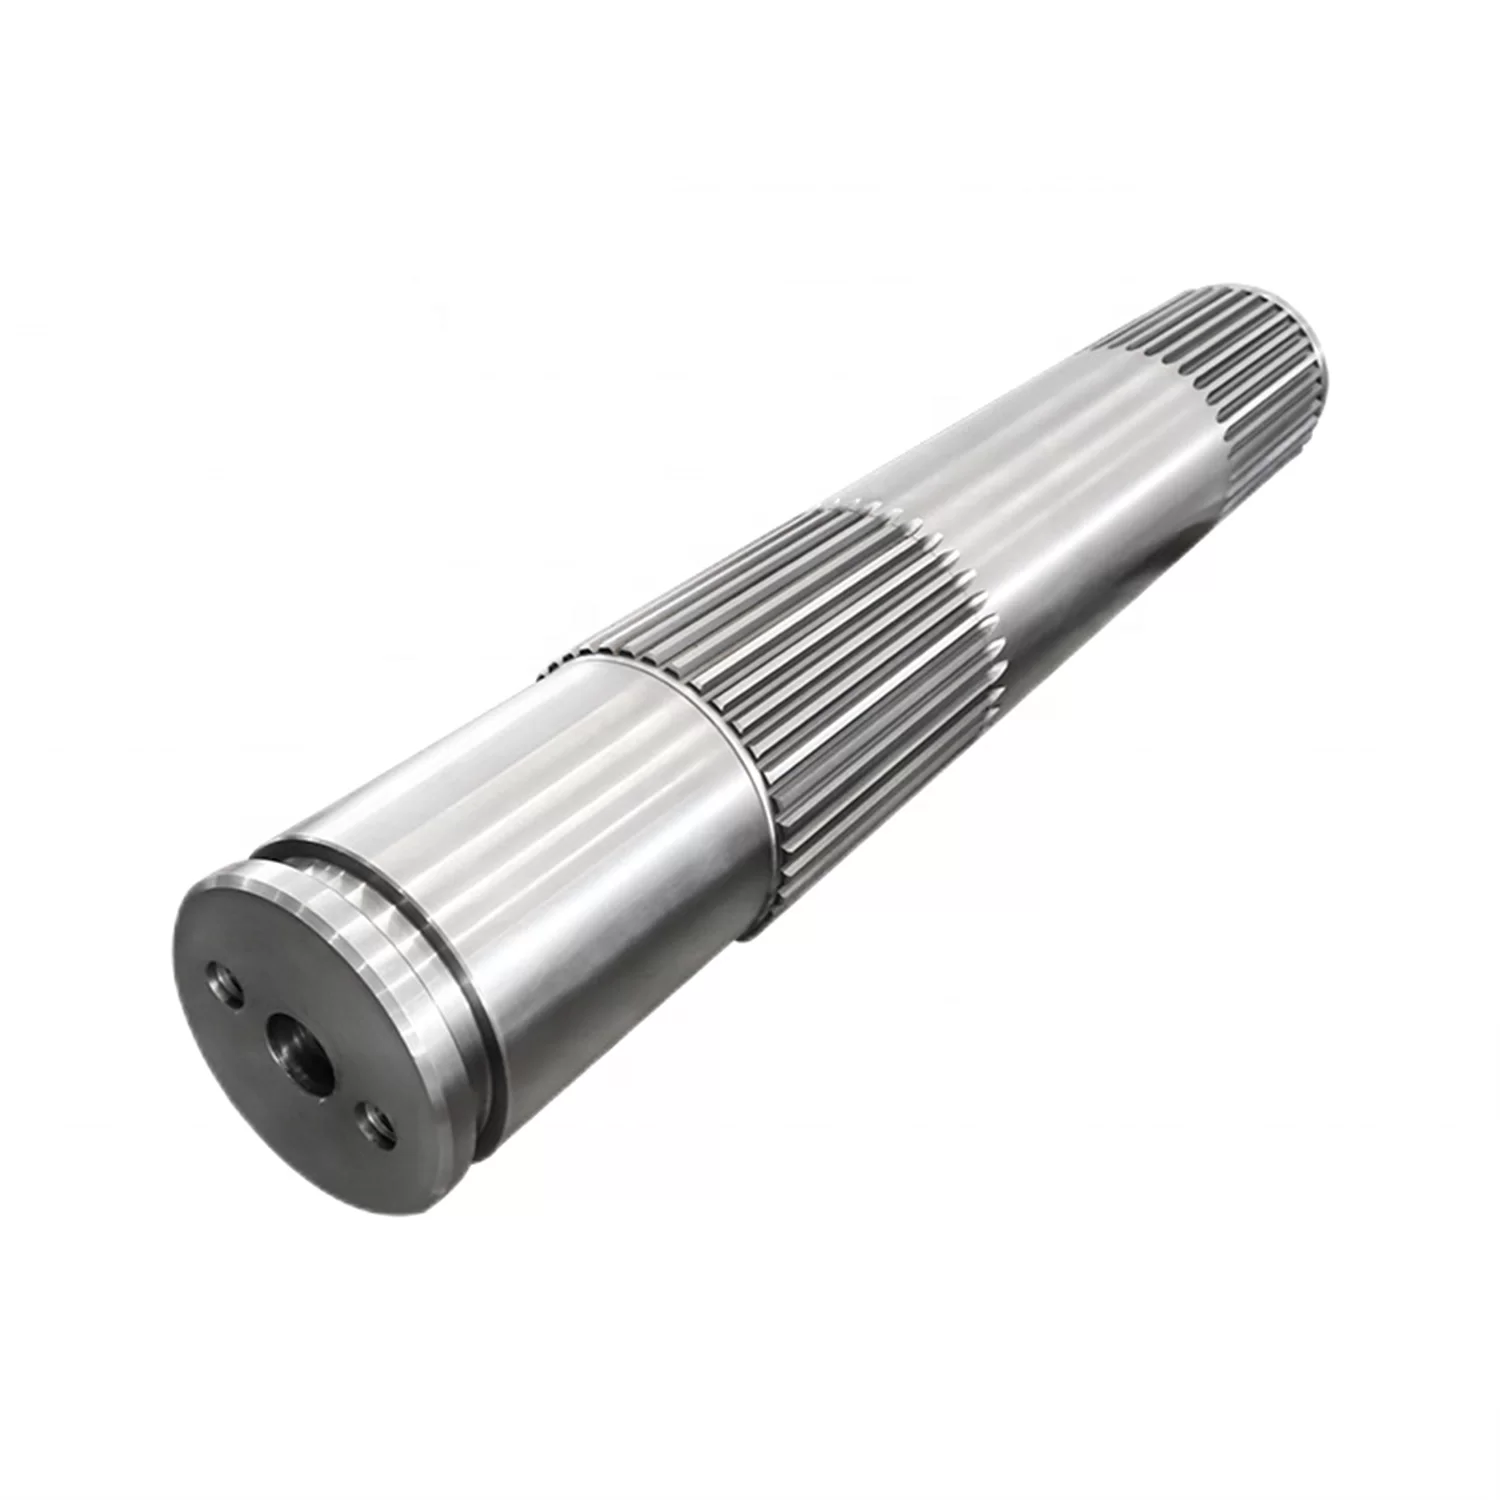 Custom Forging by Drawing
Custom forgings by drawing are produced for non-standard parts that require forged material integrity together with project-specific dimensions and machining allowance.
-
 October 08, 2026High Precision Industrial Components from Custom Forgings FactoryThe procurement of high-precision industrial components requires a deep understanding of material science and manufacturing processes. For critical applications such as heat exchanger tube sheets and pressure vessel internals, the choice between rolled plates and forged blanks is not merely a cost decision, but a structural integrity imperative. This article examines the technical advantages of utilizing a custom forgings factory to ensure the reliability of heavy-duty industrial equipment. In high-pressure environments, dimensional stability and the elimination of internal material voids are paramount. Traditional plate-based alternatives often suffer from variable homogeneity, which can lead to warping during heavy drilling and facing operations.
-
 October 05, 2026High Performance Forged Rotor Shaft Factory Precision BlanksAchieving dimensional stability and material homogeneity in heavy industrial components requires a departure from traditional plate-cutting methods. For critical applications in pressure equipment and rotating machinery, Machined Disc Blanks provide a high-performance engineering foundation. By integrating precision forging with preliminary machining, these components eliminate the inherent risks of laminated structures found in plate-based alternatives, ensuring a consistent internal grain flow that is essential for high-stress environments. These engineered blanks are designed specifically to streamline downstream production. By delivering components with optimized stock for facing, boring, and drilling, manufacturers can bypass extensive roughing stages, reducing overall cycle times while maintaining extreme machining accuracy.
-
 October 01, 2026High Quality Traceable Forgings with NDT Factory ServicesIn high-stakes industrial engineering, the integrity of a forged component is not merely a matter of dimensions but of documented certainty. For safety-critical applications, procuring traceable forgings with NDT factory capabilities ensures that every internal structure and chemical property is verified before the part ever reaches the final machining stage. This article examines the intersection of non-destructive testing NDT and process traceability in the production of heavy forged discs. For procurement officers and project engineers, the challenge lies in distinguishing between standard commercial forging and project-grade manufacturing.
-
 September 29, 2026High Quality Seamless Rolled Rings Factory for Industrial PartsA rolled rings factory specializes in the production of seamless cylindrical components created through a process of heating and rolling a metal billet. Unlike cast or welded rings, rolled rings possess a continuous grain structure that significantly enhances their mechanical properties, making them essential for high-pressure and heavy-load industrial environments. For procurement teams in the heavy machinery and energy sectors, the challenge often lies in sourcing components that can withstand extreme stress without risking structural failure. The integrity of the wall section and the precision of the bore are critical factors that determine the lifespan of hydraulic systems.
-
 September 28, 2026Top Engineering Guide for a Forged Pipe Sections FactoryHigh-performance industrial components require a level of structural integrity that cannot be achieved through casting or simple machining. Forged components, particularly those used in heavy-duty transmission and pressure systems, rely on the controlled deformation of metal to eliminate internal voids and refine the microstructure. This article examines the technical requirements for selecting a forged pipe sections factory and the engineering principles that govern the production of project-grade heavy forgings. In sectors such as power generation, oil and gas, and heavy machinery, the failure of a single forged ring or pipe section can lead to catastrophic system downtime.
-
 September 21, 2026Custom Pipe Section Forgings from Forged Flanges FactoryWhen managing high-pressure industrial assemblies, the structural integrity of tubular connectors often becomes the primary failure point. Standard cut-pipe solutions frequently fall short in complex engineered equipment where non-standard transitions and extreme wall thicknesses are required. Custom Pipe Section Forgings address these critical engineering gaps by utilizing a dedicated forging route that optimizes grain flow and enhances fatigue resistance, providing a robust alternative to fabricated piping. Designed specifically for EPC Engineering, Procurement, and Construction and OEM projects, these components ensure that critical connection zones can withstand rigorous operational stresses while maintaining precise dimensional adherence to technical drawings.
-
 September 18, 2026Reliable EPC project forgings factory for Industrial InfrastructureSecuring the integrity of large-scale industrial infrastructure requires more than just raw materials; it demands a precise synergy between engineering design and manufacturing execution. For Engineering, Procurement, and Construction EPC contractors, selecting an EPC project forgings factory is a critical decision that directly impacts the structural safety and operational lifespan of heavy-duty assets. The complexity of EPC projectsranging from offshore platforms to power plantsmeans that forgings must adhere to rigorous international standards and project-specific dossiers. Whether it is the demand for extreme torsional strength in marine propulsion shafts or the pressure containment of high-temperature nozzle necks, the manufacturing route determines the final reliability
-
 September 17, 2026High Quality EN 10204 3.1 certified forgings factory ServicesIn high-stakes industrial engineering, the integrity of forged components is not merely a preference but a safety requirement. The use of an EN 10204 3.1 certified forgings factory ensures that every piece of metal delivered to a project site comes with a verified record of its chemical and mechanical properties. This certification provides the necessary legal and technical assurance that the materials meet the specific standards required for pressure vessels, exchangers, and heavy machinery. Procurement professionals and engineers often face the challenge of balancing cost with rigorous quality control.
Sign up
for Newsletter
Subscribe to the weekly newsletter for all the latest updates


