- Tel: +86 133 3836 0365
- Email: john@yxs-forging.com
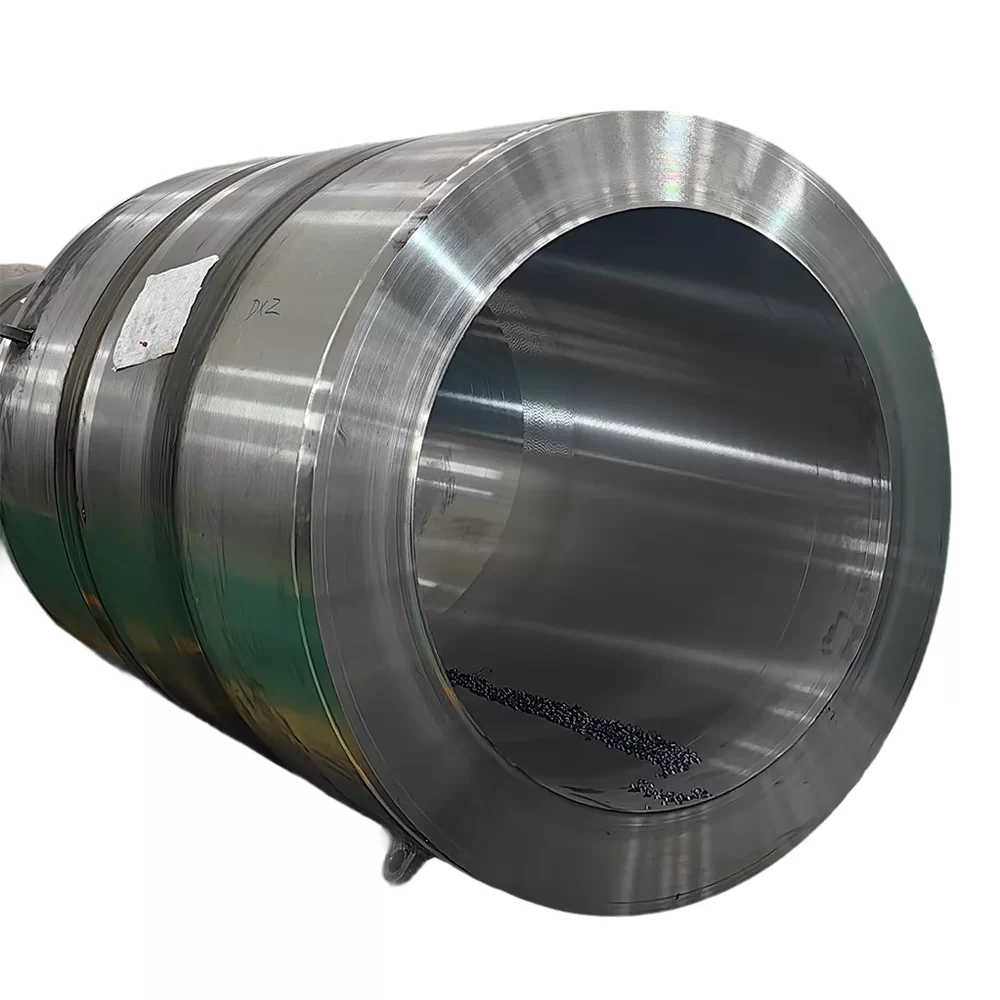
For industrial piping projects, the transition from a technical blueprint to a physical component requires more than just basic machining; it demands a rigorous adherence to dimensional compliance and material integrity. The ASME B16.5 Slip-On Flange is a critical component in pressure piping systems where installation efficiency must be balanced with strict safety standards. Whether the application involves moderate-pressure process lines or complex utility plant piping, the reliability of the flange depends heavily on its forged base and the precision of its final facing and drilling.
Procuring these components from a specialized custom forgings per drawing factory ensures that every detail—from the heat-treatment status to the NDT scope—is fully traceable and auditable. By integrating heavy forging capabilities with precision machining, manufacturers can provide flanges that meet the exact pressure class and drilling patterns required by international engineering standards, reducing the risk of onsite fitment issues and ensuring long-term operational safety in safety-critical industrial environments.

The Slip-On (SO) flange is engineered for applications where a balance between ease of installation and structural reliability is required. Unlike weld neck flanges, the SO flange slips over the pipe and is welded both inside and outside, providing a secure joint that is easier to align during field installation. This makes them a preferred choice for moderate-pressure process lines and general utility piping where the extreme stress profiles of high-pressure systems are not present.
From a technical perspective, the integrity of a slip-on flange is not determined by its simple geometry, but by its internal metallurgical structure. Forging the flange base improves material consistency and grain flow compared to casting or machining from bar stock. This structural superiority is essential for ensuring that the flange can withstand the cyclic loading and thermal expansion typical of plant piping systems without developing stress cracks or leaks at the weld interface.
Compliance with the ASME B16.5 standard is the baseline for these components. This standard dictates the precise dimensions, pressure-temperature ratings, and drilling patterns. When these flanges are produced to a specific project drawing, the focus shifts to ensuring that the bore, facing, and serrations are machined to exacting tolerances to maintain a leak-proof seal under operating conditions.

The operational environment of a piping system dictates the material grade of the flange. For carbon steel applications, A105 is the industry standard for ambient and higher-temperature service. In low-temperature environments, A350 LF2 is utilized to prevent brittle fracture. For corrosive or highly reactive media, stainless steel grades such as A182 F304, F316, or F51 are employed to ensure chemical stability and corrosion resistance.
The manufacturing process at Yongxinsheng utilizes a fully integrated system. This begins with heavy forging, where the raw ingot is shaped under high pressure to eliminate internal voids and refine the grain structure. Following forging, controlled heat treatment—such as normalizing or tempering—is applied to optimize the mechanical properties, including hardness and tensile strength, according to the project specification.
To ensure the product is fit for purpose, a comprehensive inspection regime is implemented. This includes:
Project managers and procurement engineers often face a trade-off between lead times and technical compliance. In general piping systems, a standard off-the-shelf flange may suffice. However, in project-grade installations, the "finished" look of the flange is secondary to its documentation. A project-specific dossier, including EN 10204 3.1 certificates and heat-treatment records, is mandatory for auditable quality control.
The primary application drivers for ASME B16.5 Slip-On Flanges include:
When evaluating a supplier, it is critical to verify that the manufacturer owns the entire process chain—from forging and heat treatment to final machining. This vertical integration ensures full process traceability. If a flange fails in the field, the ability to trace the part back to its original heat number and forging batch is the only way to conduct a proper root-cause analysis and prevent systemic failures across the project.
| Material Grade | Typical Application | Critical Inspection | Recommended Condition |
|---|---|---|---|
| A105 Carbon Steel | General Process Piping | Hardness / UT | Heat Treated / Machined |
| A350 LF2 | Low-Temperature Service | Charpy Impact Test | Normalized & Tempered |
| A182 F316 / F304 | Corrosive Environments | PMI / PT | Solution Annealed |
| A182 F11 / F22 | High-Temperature Steam | Mechanical Testing | Quenched & Tempered |
| Custom Alloy | Specialty Chemical Plants | Third-Party Witness | Per Project Drawing |
The difference between a generic component and a project-grade forging lies in the control system. Yongxinsheng operates under a certified framework including ISO 9001, ISO 14001, and ISO 45001, and is approved by the China Classification Society (CCS). These certifications are not merely badges but represent a commitment to a controlled and auditable manufacturing environment where every step of the forging and machining process is recorded.
Precision machining is the final critical step. The bore must be perfectly concentric to the facing to avoid stress concentrations during welding. Furthermore, the serration on the flange face—whether concentric or spiral—must be machined to the correct roughness (Ra) to ensure that the gasket creates a perfect seal under the specified bolt torque. Inconsistent machining in these areas is a leading cause of flange leaks in industrial plants.
By providing options for rough-machined blanks or fully finished semi-finished parts, manufacturers can support different process routes. For high-precision orders, additional journal machining or specific beveling can be incorporated before shipment, ensuring the component arrives at the site ready for immediate integration into the piping network.
As global industrial projects become more complex, the shift toward sourcing from a specialized custom forgings per drawing factory is accelerating. The ability to handle "project-grade" requirements—meaning the product is built to a specific engineering dossier rather than a generic catalog—reduces the total cost of ownership by eliminating the need for extensive onsite rework and reducing the probability of failure during hydro tests.
Future trends in forging indicate a move toward tighter tolerances and more exotic material combinations to meet the demands of carbon capture, hydrogen transport, and advanced petrochemical processing. Suppliers who can provide seamless coordination between the engineering arm and the manufacturing base are better positioned to support these evolving needs. The key is the ability to translate a complex drawing into a physical part while maintaining a transparent, auditable trail of quality evidence.
Ultimately, the selection of a forging partner should be based on their ability to manage the intersection of metallurgy, machining, and documentation. When these three elements are aligned, the resulting ASME B16.5 Slip-On Flanges provide the necessary confidence for safety-critical applications in the most demanding industrial environments worldwide.
Forged flanges are produced by applying compressive force to the metal, which refines the grain structure and eliminates internal porosity. This results in significantly higher strength, better fatigue resistance, and superior pressure-bearing capabilities compared to cast flanges, which may have internal voids or inconsistent material density.
EN 10204 3.1 is a material certificate that confirms the product complies with the order requirements. It includes a declaration from the manufacturer's authorized inspection representative, providing traceability to the original heat number and verifying that the chemical and mechanical properties meet the specified standard.
For low-temperature services, A350 LF2 is commonly specified. This carbon steel grade is designed to maintain toughness and resist brittle fracture at sub-zero temperatures, whereas standard A105 would be susceptible to cracking in the same environment.
Slip-on flanges are generally intended for moderate-pressure applications. For very high-pressure or safety-critical services where maximum strength and leak prevention are required, Weld Neck (WN) flanges are typically preferred due to their reinforced hub and superior stress distribution.
Positive Material Identification (PMI) uses X-ray fluorescence or optical emission spectroscopy to verify the chemical composition of the alloy. This ensures that the correct grade (e.g., F316 vs F304) was used, preventing costly mistakes and potential failures due to incorrect corrosion resistance.
You should clearly specify the facing type (RF, FF, etc.), the serration finish (e.g., 125-250 AARH), the bore diameter, drilling patterns, and any specific beveling or tapping requirements to ensure the flange fits perfectly with your existing piping and gaskets.
For detailed technical consultations regarding customized forging solutions or project-specific ASME B16.5 flange requirements, our engineering team is available to provide comprehensive support from drawing review to final verification.